
Views: 0 Author: Site Editor Publish Time: 2026-08-01 Origin: Site


Image Source: pexels
As buyers and engineers, you face big risks. Buying metal parts is hard. Picking a bad Die Casting Manufacturer causes tool breaks. It also causes high porosity and big delays.
Meanwhile, steady growth marks the global aluminum die casting market:
Metric | Value |
|---|---|
Market Valuation (2026 Estimate) | $89.3 Billion |
Projected Valuation (2033) | $134.1 Billion |
You must check top aluminum die casting suppliers carefully. Use four main steps. Check engineering skill. Look at quality passes. Review machine size. Demand clear costs. Vetting a leading aluminum Die Casting Manufacturer shields your supply chain. You get good aluminum die casting by checking skills. Also check quality systems. Reviewing machine capacity ensures smooth aluminum die casting for all orders. Plus, buying teams need a trustworthy Die Casting Manufacturer to cut wait times. Following this top guide brings strong aluminum die casting. It works for structural aluminum parts. It also works for light aluminum housings.
Check engineering skills early.
This improves part designs.
It stops costly product breaks.
Verify quality certs like ISO 9001.
This ensures strong parts.
It keeps production very steady.
Match part and machine sizes.
This avoids defects and leaks.
Review total spend numbers.
Look beyond basic part costs.
This helps manage your budget.
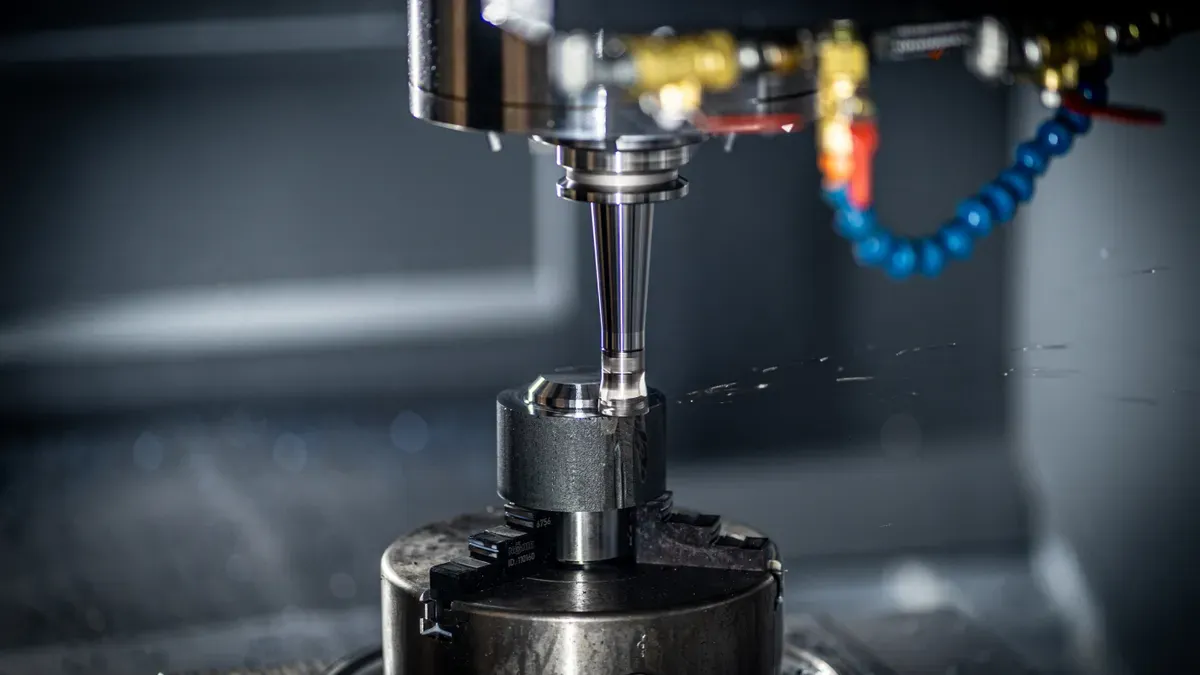
Image Source: pexels
You must check a factory's engineering skill first. Good skills help make more good parts. Modern shops use special vacuums to pull air out. They also track machines live during production runs. These tools stop inside holes. They keep parts accurate. Thus, your supplier makes fewer bad parts. Factory output stays very high. Checking these skills brings success to your big jobs.
Key Takeaway: Early checks stop costly field breaks later. Find suppliers that give design help. Seek good metal knowledge. Look for tool care and right press choices.
Work with a skilled team early. This stops long delays later. You need early design advice before making molds. Computer tests show trapped air. They check cooling paths. They also fix metal entry points. Early reviews make metal freeze evenly. This stops holes. It removes extra fix work.
[Design Phase Review] ➔ [Mold Flow Simulation] ➔ [Defect Identification] ➔ [Tooling Optimization]
Good layout rules keep your aluminum parts very strong:
Uniform Wall Thickness: Keep walls even between 1.5 mm and 3.0 mm. Even walls help metal flow fast. Metal freezes fast too. Change thickness very slowly.
Rib Implementation: Add ribs on wide parts. Ribs add strength. Space ribs in odd counts. This stops stress on nearby spots. Make ribs thin to stop surface dips.
Draft Angles and Radii: Put small angles on outer walls. Use bigger angles inside. Smooth corners stop tears. They stop tool wear too.
Good rules make metal flow well in casting. Doing this early gives better casting results.
Your shop must help pick the best metal. Different uses need different strength. They need heat control. They need rust protection too.
Alloy | Mechanical & Performance Characteristics | Casting & Flow Properties | Primary Trade-offs |
|---|---|---|---|
A380 | Good strength. Balanced overall performance. | Flows well. Fills molds easily. | Normal rust defense. Normal pressure hold. |
ADC12 | Holds exact shape well. Reliable strength. | Great mold filling. Good for thin parts. | Needs coatings to stop rust well. |
A360 | Great rust defense. Better pressure hold. | Flows slower. Sticks to molds easily. | Needs extra care during work. |
Mix items change metal behavior:
Chemical Element | ADC12 Range (%) | A380 Range (%) | Influence on Material Properties |
|---|---|---|---|
Silicon (Si) | 9.6 – 12.0 | 7.5 – 9.5 | Helps metal flow. Boosts wear strength. |
Aluminum (Al) | Balance | Balance | Main light metal. Gives basic rust defense. |
Standard metals fit most frame parts. High-tech jobs need special metals. Mixed aluminum brings great heat flow. It gives high strength for car engines. Also, 5000 and 6000 metals stop rust. They work for car frames and boats. The 1000 type moves heat best.
Tool design guides metal paths and part removal. Gates balance filling. They cut air bubbles. They fix cold spots. Changing gate shapes cuts hot spots in half. Good pins stop part bending and marks.
Planned tool care grows mold life. It protects part shapes. Work without care causes heat shock. Heat shock cracks tool steel fast.
Frequency | Operational Tasks | Maintenance Goal |
|---|---|---|
Daily (Every Shift) | Clean mold joints. Grease moving pins. Stop extra metal. | Avoid work stops. Keep use safe. |
Weekly (5,000 Cycles) | Clean center parts. Check pins. Clear vent paths. | Stop buildup. Lower pin wear. |
Major Service (25,000 Cycles) | Take apart slides. Polish spaces. Check liquid lines. | Fix early wear. Keep cooling fast. |
Shops must set cool lines for steady heat. Adding thin outer coats boosts wear life. Scheduled fixes keep tools accurate. This brings high work speed for every casting run.
Match your part shape to machine size. Wrong machine size causes liquid leaks. It causes bad sizes. Parts stay incomplete. Engineers find needed clamping force with easy steps:
Determine Total Projected Area: Measure top flat area at mold line. Add main part, channels, and extra spaces.
Establish Injection Pressure: Pick force based on wall thickness. Thin walls need high push force.
Compute Base Clamping Force: Multiply total area by target metal push.
Factor in Safety Margin: Multiply base force to cover shop changes.
Different part sizes need matching press sizes:
1650T – 2500T Presses: Make mid-sized parts like gear cases.
3050T Presses: Make big parts like battery boxes.
4000T+ Presses: Handle huge car parts.
6000T to 9000T Gigacasting Presses: Cast whole car bottoms. They replace many welded parts.
Checking press size ensures suppliers handle all orders. Finding press space builds total trust. You get good parts on time.
You need top quality systems. Good quality protects your brand name. It stops part breaks too. Checking systems keeps your project safe.
Certifications show basic factory skills. Global buyers need them for jobs. Check these rules first:
ISO 9001:2015: This sets basic factory rules. It keeps part sizes steady.
IATF 16949: This covers car part rules. It keeps metal parts safe.
Getting these badges helps aluminum casting plants. Badges show great work. They bring clear gains:
Better quality management daily.
Fewer broken parts and less risk.
Less wasted metal in shops.
Good parts made to your rules.
Better work speed and happy buyers.
Top shops use these rules everywhere. Certified plants track every metal melt.
Special tools check your metal parts. Demand three main tests from suppliers:
Quality Control Method | Specific Function & Capabilities | Quality Assurance Impact | Primary Role in Production |
|---|---|---|---|
CMM Dimensional Analysis | Measures down to 0.0001 inches. It builds 3D models. | Finds bad sizes fast. It confirms shapes early. | Checks part size limits fast. It stops extra machine costs. |
Spectrographic / Quantometer Analysis | Checks metal elements fast in alloys. | Checks real metal traits. It matches standard rules. | Checks liquid metal daily. It lets workers fix mix. It cuts scrap by 22%. |
X-ray tools check inside parts too. The test sends rays through metal:
Dense metal stops rays. It makes dark spots.
Air holes let rays pass. They make bright spots.
The test film saves inside records.
Digital X-ray tools find hidden holes early.
Test physical samples before full production. Use these four steps during testing:
Request Relevant Samples: Ask for real sample parts. Match your needed shape skill.
Perform Independent Testing: Test parts in your shop. Check metal strength and size.
Assess Technical Responsiveness: Watch how shops fix design issues. Check their speed and help.
Verify Rapid Prototyping Capabilities: Check for fast sample tools. Quick tools speed up turns.
Real samples show surface marks fast. Testing parts confirms true strength early.
Holes weaken parts and cause leaks. A good die casting manufacturer stops holes:
Porosity Category | Primary Causes | Prevention & Control Measures |
|---|---|---|
Gas Porosity | Trapped air from fast flows. Poor mold vents. Extra lube gas. Wet tools. | Use vacuums in molds. Clean metal with gas. Keep vents clean. Smooth inner corners. Use auto sprays. |
Shrinkage Porosity | Metal shrinks while cooling. Uneven wall size. Poor metal push. Early gate freezes. | Make even wall sizes. Use extra squeeze force. Fix injection speeds. Set right wall angles. Pick easy-flow metals like A380 or ADC12. |
New shops use vacuums to pull air out:
Vacuum Mechanism | Operational Effect | Impact on Defect Elimination |
|---|---|---|
Pre-injection evacuation | Lowers air pressure in molds. | Fills molds tight. It removes air pockets. |
Continuous air extraction | Keeps metal flowing smooth. | Stops trapped gas. It creates strong parts. |
Powered vacuum pumping | Helps liquid metal flow better. | Adds part strength. It removes surface holes. |
Vacuums pull air from molds fast. Removing gas cuts internal air holes. Picking a smart shop ensures good parts.
New shops use robots to speed up work. Robots handle every step very well.
Automation Mechanism | Impact on Cycle Time | Impact on Production Consistency |
|---|---|---|
Robotic Motion & Handling | Cuts cycle times with quick moves. | Keeps part sizes steady in big runs. |
Continuous Flow Integration | Cuts stops during metal feeding and removal. | Fixes heat shifts and timing mistakes. |
Automated Ladling & Feeding | Cuts wait times during metal feeding. | Pours exact metal amounts at steady speeds. |
Smart machines match action times. They speed up part removals. This plan boosts big runs. It keeps parts very exact. A top shop uses aluminum die casting for steady parts.
Track shop schedules to protect your project. Knowing each step stops costly delays.
Production Phase | Estimated Duration |
|---|---|
Tooling Fabrication (Rapid/Sampling) | 10–15 business days |
Tooling Fabrication (Production/Hardened) | 4–8 weeks |
Initial Run / T1 Sampling | 5–15 business days |
Full Mass Production Cycle | 4–8 weeks |
Good partners finish every aluminum die casting job on time. They run schedules with clear views. You can plan item launches with full trust.
Rough aluminum die casting parts need extra work. CNC tools reach tight sizes. They fix parts within ±0.01 mm to ±0.05 mm. This step gives rough parts sharp sizes. Cuts reach as tight as ±0.001 inches.
Shops add many outer coats to metal parts:
Anodizing: Boosts rust defense and outer hardness.
E-Coating: Works as a low-cost outer coat.
Powder Coating: Adds a safe, strong outer layer.
Shot Blasting: Cleans rough metal surfaces first.
Picking full finishing choices saves project money.
A strong supply line stops work delays. Your aluminum die casting supplier must hold raw metal stock. They run each aluminum die casting job with backup plans.
Also, top suppliers check aluminum die casting tools to stop work stops. They balance machine space to raise shop output. You get reliable shipments for every aluminum die casting order. Smart plants make great aluminum die casting parts daily. Good shops protect your aluminum die casting plan at every step. You gain great outcomes with dedicated aluminum die casting support.
Buying teams must track full spending numbers well. Looking only at item costs tricks you. Reviewing all money needs helps save cash. It aids your factory business over time.
Ask your aluminum die casting shops for clear lists. Good makers split tool fees from part costs. You must check run times alone. Check labor fees and raw metal rates too. Clear aluminum die casting cost plans stop surprise price jumps.
Metal prices change each day on public markets. Top shops link part prices to market rates. This open aluminum die casting pricing plan stays fair. Safe price rules keep production budgets steady. They protect long sales deals over many years.
Set mold owner rights before sending early money. Your paper must state you own tools fully. Great shops cover mold life for set runs. These runs often reach 100,000 shots. The shop fixes or swaps worn tools. This spending helps keep work moving fast.
Smart buyers find the full expense past base prices.
Cost Category | Factors to Include in TCO |
|---|---|
Direct Manufacturing & Materials | • Raw aluminum material |
Post-Processing & Quality | • Secondary operations (finishing, machining, coating) |
Operations & Lifecycle | • Overhead costs (energy consumption, machine maintenance) |
TCO Insight: Put these vital spends in your plan budget:
Landed & Logistics Costs: Cover packing, shipping, tariffs, insurance, and fees for tracking foreign vendors.
Inventory & Carrying Costs: Account for goods sitting in storage or moving.
Contingency Buffer: Keep safety funds (5% to 15%) for unexpected project costs.
Checking these points brings great aluminum die casting results. You guard factory work and raise overall metal returns.
Picking good metal casting shops needs four steps. Check tech skills. Look at quality rules. Check plant size. Review total costs. Ask for a free design test first. Get sample parts before you pick one shop.
RFQ Audit Category | Key Parameters to Evaluate |
|---|---|
Machine Capability | Press power and metal shop health |
Quality Systems | Size tools, metal tests, and ray checks |
Smart partners help your metal casting work. Always test raw metal fast. Ask for a design review now. Our team makes great metal parts for you. We use proven casting ways daily.
Procurement Tip: Send 3D models early. Get quick design checks before signing.
Ask for ISO 9001 rules first. Car parts need IATF 16949 rules. These global standards ensure your die casting manufacturer controls steps. They lower bad parts. They bring good batches always.
Stop inside holes using vacuum systems. Top shops use fast valves. They use clean mold vents. They track shots live. These tools pull trapped air out fast. Liquid metal fills molds cleanly then.
Part shapes change mold speeds. Surface needs change speeds too. Steel choices matter a lot. Easy test molds take two weeks. Hard full molds take eight weeks. Early reviews stop extra work fast.
A380 metal works best for most jobs. It flows fast into thin spots. It cools down quickly too. For wet outdoor spots, pick A360 metal. It stops rust very well. It holds pressure tight.
Extra CNC cuts raise item prices. Surface coats add extra fees. You must check total costs early. Doing casting and finishing together cuts shipping risks. It guards your supply money well.
